KORRETTO · Lathe center series
Medium-Duty Live Center
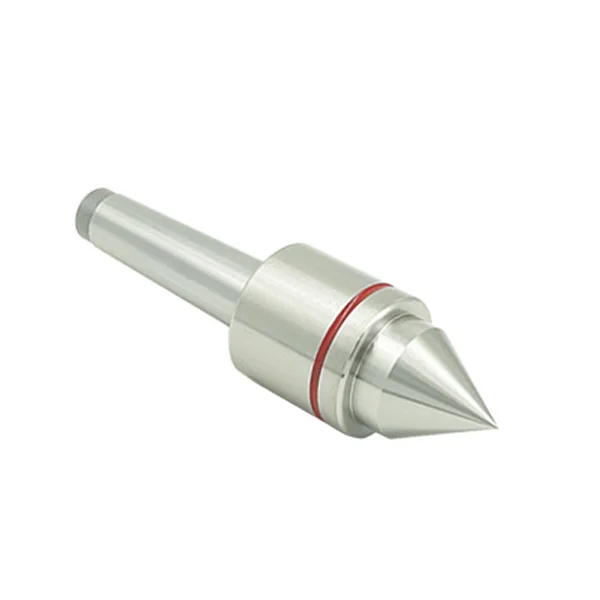
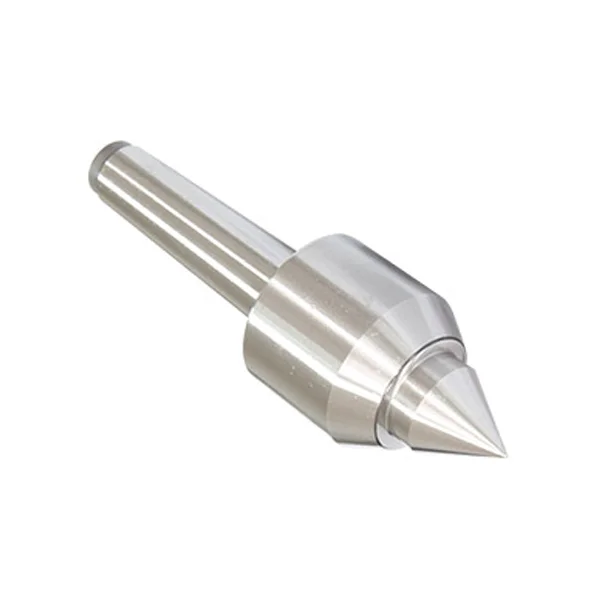
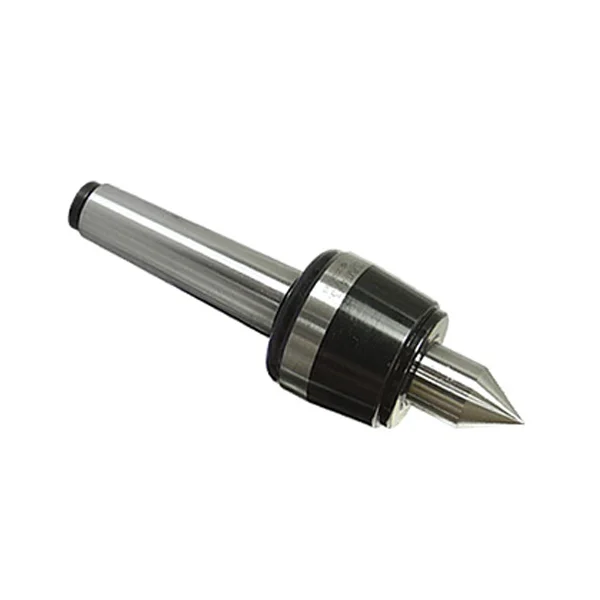
Medium-duty live centers provide balanced support capacity for common shaft and sleeve parts. They are suitable for medium-load turning applications where stability, service life and tailstock support must be considered together.
Send the Morse taper, workpiece weight, machining speed, center hole size and whether a dustproof or oiling structure is required, and we will help check the suitable medium-duty live center series.
Product Overview
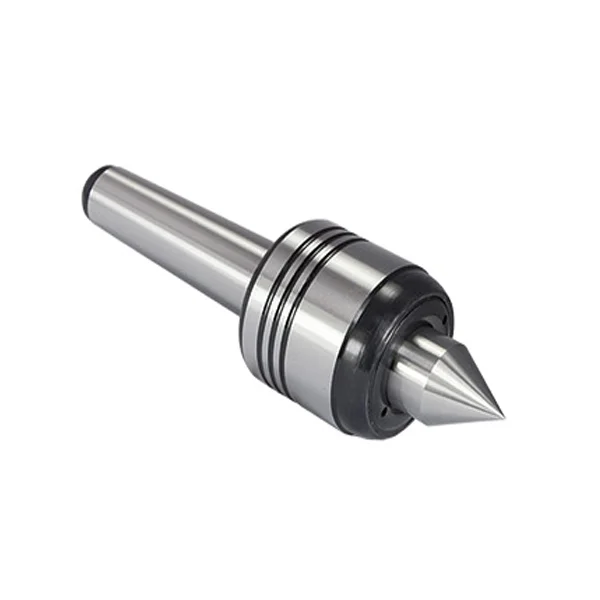
The C011 and C021 medium-duty live centers support shaft and sleeve workpieces from the lathe tailstock. C011 is the standard series. C021 adds the dustproof / oiling structure listed in the second table. Select the series and Morse taper together.
How a Medium-Duty Live Center Works
The Morse-taper shank locates the center body in the lathe tailstock while the center spindle rotates on its internal bearings with the workpiece. The point supports the workpiece through its center hole, so the bearings carry the resulting axial and radial loads while reducing sliding friction at the contact point. Actual support performance depends on taper fit, center-hole condition, tailstock pressure, workpiece weight, cutting force and operating speed.
Typical Applications
- Medium-load shaft turning
- Sleeve and shaft-type workpieces
- General lathe tailstock support
- Batch machining with repeatable support requirements
- Applications requiring MT2 to MT6 live center options
Key Features
Medium-duty live center structure
Covers standard C011 series and dustproof / oiling C021 series
Suitable for MT2 to MT6 tailstock interfaces
Balanced load capacity for general turning
Stable rotating support for medium-load workpieces
Parameters and Dimensions
Use the dimension drawing and parameter tables below to verify taper size, dimensions, speed, accuracy and support load before model selection.

| Order No. | Model | D (mm) | D1 (mm) | D2 (mm) | L1 (mm) | L2 (mm) | L (mm) | Max. RPM | Accuracy (mm) | Workpiece Weight (kg) | Net Weight (kg) |
|---|---|---|---|---|---|---|---|---|---|---|---|
| C011010 | BZ-MT.2 | 17.78 | 45 | 22 | 80 | 32 | 148 | 2500 | 0.008 | 400 | 0.80 |
| C011110 | BZ-MT.3 | 23.825 | 53 | 26 | 84 | 32 | 170 | 2500 | 0.008 | 500 | 1.28 |
| C011210 | BZ-MT.4 | 31.267 | 63 | 30 | 104 | 39 | 212 | 2000 | 0.008 | 600 | 2.20 |
| C011310 | BZ-MT.5 | 44.399 | 78 | 44 | 136 | 53 | 260 | 2000 | 0.008 | 600 | 4.33 |
| C011410 | BZ-MT.6 | 63.348 | 128 | 70 | 190 | 80 | 379 | 2000 | 0.008 | 700 | 14.20 |
| Order No. | Model | D (mm) | D1 (mm) | D2 (mm) | L1 (mm) | L2 (mm) | L (mm) | Max. RPM | Accuracy (mm) | Workpiece Weight (kg) | Net Weight (kg) |
|---|---|---|---|---|---|---|---|---|---|---|---|
| C021010 | BZ-MT.3 | 23.825 | 53 | 23 | 87 | 32 | 170 | 2000 | 0.008 | 500 | 1.15 |
| C021110 | BZ-MT.4 | 31.267 | 63 | 28 | 115 | 40 | 225 | 2000 | 0.008 | 600 | 2.5 |
| C021210 | BZ-MT.5 | 44.399 | 78 | 36 | 135 | 50 | 270 | 2000 | 0.008 | 600 | 4.30 |
| C021310 | BZ-MT.6 | 63.348 | 128 | 70 | 190 | 80 | 379 | 2000 | 0.008 | 700 | 14.2 |
Image Gallery
Selection Notes
Check the tailstock taper before comparing loads. The C011 table covers MT2 to MT6; C021 starts at MT3. A matching taper seats the center body in the tailstock and keeps the support axis aligned with the workpiece.
Compare the model rows at the required working speed. For example, the MT3 C011 model lists 2500 rpm, while the MT3 C021 model lists 2000 rpm. Both rows list a workpiece weight of 500 kg. These are model values, so keep speed and load from the same row.
Use the standard series for general shaft turning. Review C021 when the setup needs its dustproof / oiling structure. For different center-hole shapes on the same body, compare the live center with interchangeable inserts.
When a Medium-Duty Live Center Is Not Suitable
Do not select this series when the required workpiece weight or RPM exceeds the limit shown for the chosen model, when the tailstock taper is not confirmed, or when the workpiece has a damaged, shallow or off-center center hole. Heavy cutting loads may require a heavy-duty or high-load center, while sustained high-speed or coolant-intensive machining may require a dedicated high-speed sealed design. Keep a practical margin below the published load and speed limits and confirm the final choice against the actual process.
FAQ
What is a medium-duty live center used for?
A medium-duty live center is used for rotating tailstock support of workpieces that are larger than light-duty applications but do not require a heavy-duty center. It is suitable for general-purpose turning support with moderate load conditions.
Is it a live center or a dead center?
It is a live center. The center rotates with the workpiece and is selected for medium support loads in turning operations.
What machine taper should be confirmed?
Please confirm the tailstock taper or machine center interface before selection. The medium-duty live center must match the machine taper correctly.
What workpiece weight or support condition should be checked?
Please confirm the workpiece weight, shaft length, center-hole size and support load. These factors determine whether the medium-duty class is suitable.
What speed or load should be considered?
Please confirm the operating speed and support load. The center should be selected according to the actual machining condition and not only by workpiece diameter.
How is it different from light-duty or heavy-duty live centers?
A medium-duty live center fills the range between lighter general work and heavier shaft support conditions. Final choice depends on the actual support load, speed and workpiece size.
What should be checked before installation?
Check the taper fit, center-hole condition, support alignment and operating speed before installation. The contact surfaces should be clean and correctly matched.
What information is needed for quotation?
Please provide the machine taper, workpiece weight, shaft length, center-hole size, speed range and machining process.