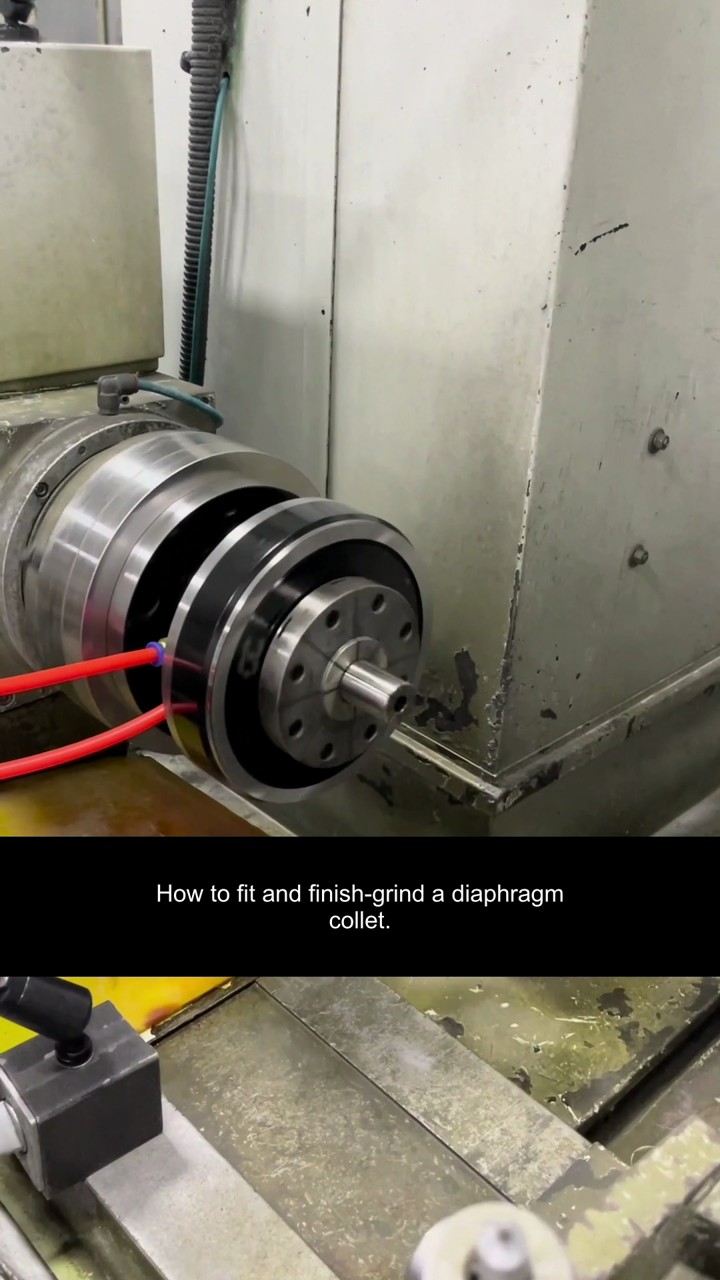
How to Fit and Finish-Grind a Diaphragm Collet
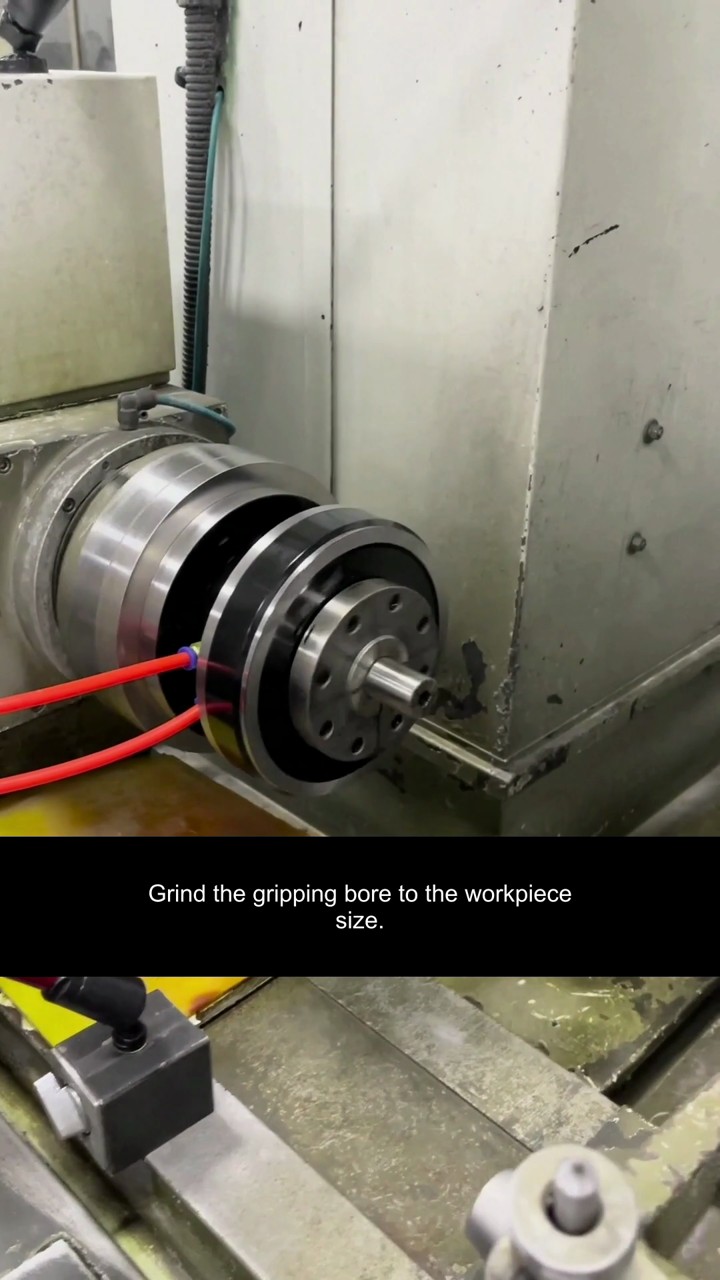
This tutorial follows the setup from mounting the chuck to finish-grinding its diaphragm collet. Mount the chuck on the spindle flange and check the radial and face datums. Fit the diaphragm, secure its screws and set the air pressure before grinding the gripping bore. The chuck shown is a JA6-100.
How the grip works
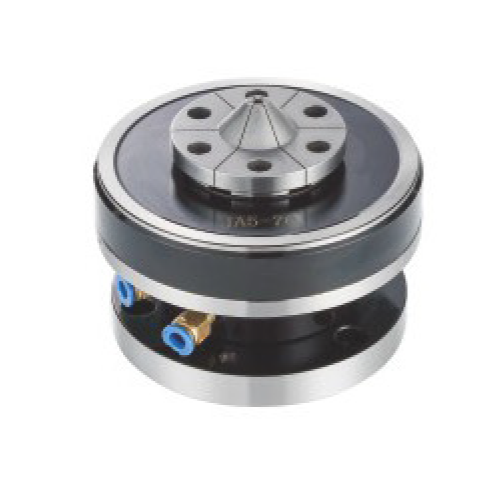
The built-in pneumatic cylinder flexes a metal diaphragm. Its gripping segments move with that small elastic deflection. The grip does not depend on conventional jaws travelling along long slideways. A replaceable diaphragm collet is finished to match the part. External gripping closes onto the outside diameter. Internal gripping expands against the bore.
Choose the gripping direction from the machining datum. Gripping inside a bore leaves the outside diameter accessible. For a slender shaft or thin wall, set the contact length, overhang and clamping force together. After mounting, check the chuck datum first, then the gripped part.
What to check in this setup
- Apply air to open the locating register, then align the diaphragm holes.
- Shut off and disconnect the air before fastening the diaphragm screws.
- This finish-grinding demonstration uses 0.1 MPa, then grinds to the workpiece size.