Customer Test: Clamping Head Chuck Runout at the Far End of a Small-Diameter Workpiece
The customer measures near the free end
This customer is testing our clamping head chuck on a small-diameter part. The part extends out from the head, and the indicator touches it near the free end. That measuring position is the main point of this video: the customer is checking away from the chuck face.
How the customer checks the part
The customer fixes the indicator on a holder, places its tip against the outside of the part and turns the chuck by hand. The camera then moves closer to the dial, making the measuring position and reading process easier to see.
Watch the customer test on YouTube
Why measure farther from the chuck?
A measuring point farther from the grip makes a tilted workpiece axis easier to spot. The same small angle produces a larger radial change over a longer projection. For a shaft that will be machined near its free end, a reading there is especially useful.
Slender parts are also affected by gripping length, contact position and outside forces. Measure near the chuck and near the free end without changing the grip. Comparing the two readings helps you look at radial offset and the direction of the part axis.
What to read over one revolution
Over a full revolution, note the highest and lowest readings. Their difference is the total indicated runout, or TIR, at that point. The 0.01 mm marking on the dial is the graduation per division. Also record how far the measuring point is from the grip.
What actually grips the part?
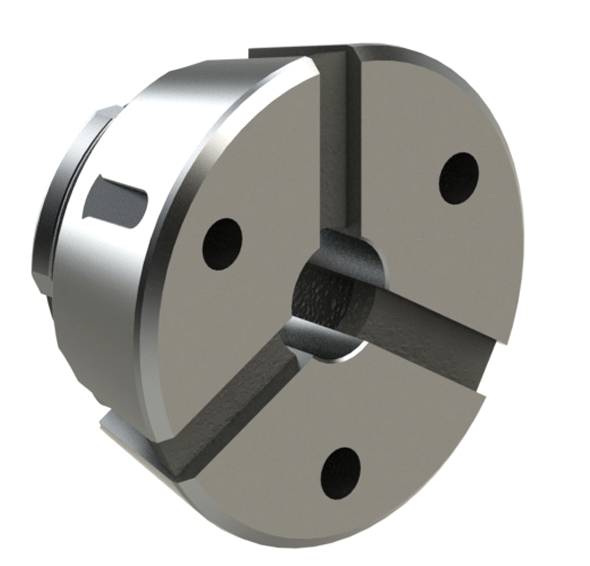
The rubber does not directly grip the part. Hardened steel segments provide the gripping faces. Vulcanized rubber joins those segments so they open and close together, and fills the gaps. Axial movement against the taper in the matching chuck closes the head around the part.
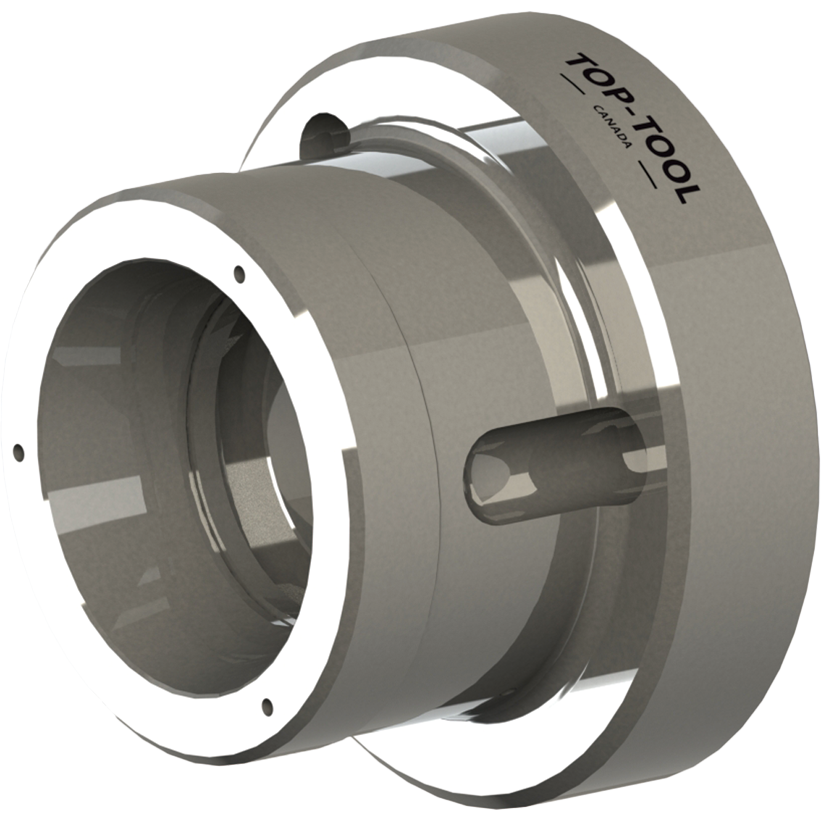
The chuck stays on the machine, while the head is chosen for the part size. For a different component, you can change the matching head without removing the chuck. Label each head with its reference, bore size and contact length so it is easy to find for the next job.
Gripping length and overhang
Plan gripping length and projection together: how much of the part sits inside the head, and how much needs to remain accessible for cutting and measuring? A stop or locating face sets the loading depth. Keep the holder steady and avoid heavy sideways tip pressure on a slender part.
Reload the part and compare
Before checking the first part, clean the mating and gripping surfaces, fit the correct head and load the part against its reference. Clamp it, then check rotation. Keep the measuring point, loading depth and clamping settings the same for the following parts.
To check repeat clamping, release the same part, take it out and reload it, then compare the readings. Keep the measuring point and clamping settings unchanged. The changing tool removes and installs the head; the bore tool prepares a machinable head. They do different jobs.
Related chucks, heads and tools
The links below show the chuck, heads and tools used in this type of setup. Check the gripping profile alongside the chuck connection, changing tool and bore tool.
- Clamping Head Systems
- Through-Hole Clamping Head Chuck
- Segmented Clamping Head
- Clamping Head Changeover Tool
- Clamping Head Bore Tool
Does your part need a far-end check?
If your part needs machining farther from the chuck, send us the drawing with gripping diameter, tolerance, gripping length, projection and measuring distance. Add the material, machine connection and operations so we can discuss the head, location and inspection setup.